What Is a Multi Axis CNC Machine and How Does It Work?

A multi axis CNC machine removes material with coordinated cutting movements. Unlike a traditional three-axis system, it can rotate the workpiece or spindle. This added motion reaches angled surfaces, deep cavities, and complex contours with fewer setups. The result can be a more accurate part and a cleaner production workflow.

The term Cnc Machine Multi Axis usually describes equipment with four, five, or more controlled axes. Each axis follows programmed coordinates from CAD and CAM software. The controller converts those instructions into synchronized motor movements. Linear axes guide the tool along X, Y, and Z. Rotary axes tilt or turn the cutting tool, table, or workpiece. A five-axis machine may cut several surfaces during one clamping operation. That detail matters. Repositioning can introduce alignment errors and consume valuable shop time.

In practice, successful machining depends on more than axis count. Tool length, spindle speed, cutting force, fixture design, and material behavior all affect the final result. An experienced operator checks simulations before machining expensive aluminum, steel, or titanium stock. They also inspect tool clearance and verify the work coordinate system. A small programming mistake can damage a tool quickly. It can also spoil an entire batch. Multi-axis equipment is powerful, but it is not automatically better for every component. A simple bracket may cost less on a three-axis machine. This is where planning needs honest review. The best choice balances geometry, tolerance, volume, operator skill, and maintenance requirements.
What Is a Multi Axis CNC Machine and How Does It Work?

Definition and Core Principles of Multi-Axis CNC Machining

What Is a Multi Axis CNC Machine and How Does It Work?

A multi-axis CNC machine controls cutting tools along several coordinated directions. Most systems use X, Y, and Z linear axes, with rotary A, B, or C axes added. The core principle is coordinated motion. Several axes move together.

In three-axis machining, the tool usually approaches a part from one direction. Multi-axis machining can tilt or rotate the tool around complex surfaces. This access reduces repeated setups and helps produce undercuts, curved housings, and angled holes. In 3+2 machining, rotary axes position the workpiece before cutting. In simultaneous five-axis machining, all axes can move during cutting.

A CNC controller reads toolpaths created from digital part data. It calculates machine movements, tool angles, feed rates, and cutting locations. Kinematic calculations matter because rotary motion changes the tool’s actual position. A small setup error can create visible surface marks or dimensional drift. Real production work also depends on probing, tool-length measurement, rigid workholding, and regular calibration. The machine is precise, but not magically perfect.

Experienced machinists still check the first component carefully. They compare critical dimensions with inspection equipment and adjust offsets when needed. Tool wear, vibration, and heat can change results.

The term “multi-axis” can sound complete, yet machine configuration and programming quality often matter more than axis count. That detail deserves attention.

Main Machine Components and Their Functions

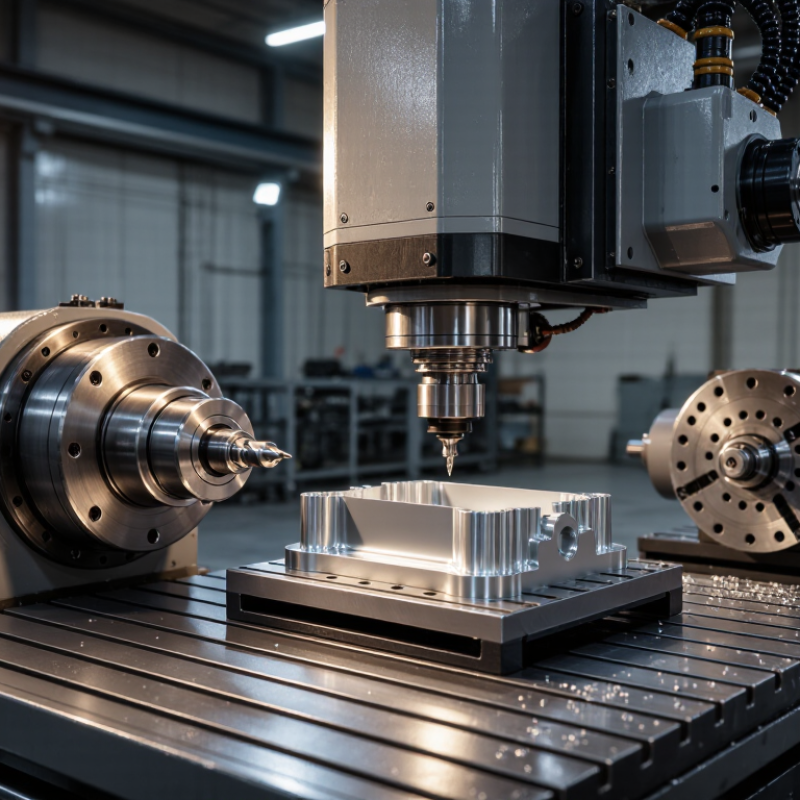
A multi-axis CNC machine removes material by coordinating several controlled movements. Its frame supports the cutting forces and reduces vibration during machining. The spindle holds and rotates the cutting tool at a programmed speed. Axis motors move the tool or workpiece along linear paths, while rotary axes tilt or rotate the part.

The CNC controller acts as the machine’s decision center. It reads programmed coordinates, adjusts motion commands, and synchronizes spindle speed with feed rate. Servo drives convert these commands into accurate movement. In practical machining, even a small positioning error can affect hole locations or surface finish. Alignment matters.

A rotary table or tilting head exposes several part faces without repeated setups. This can improve accuracy and shorten production time. The tool magazine and automatic changer select different cutters during one cycle. Coolant carries heat and chips away from the cutting zone. A probing system checks workpiece position, tool length, and sometimes finished dimensions.

Workholding remains a critical component. A rigid fixture prevents movement, but excessive clamping force can distort thin parts. Heat changes everything. Experienced operators verify tool wear, fixture stability, and calibration before trusting a long cycle. Still, no setup is perfect; vibration, chip buildup, or thermal growth may require adjustments during production.

How Multi-Axis CNC Machines Coordinate Tool Movement

What Is a Multi Axis CNC Machine and How Does It Work?

How Multi-Axis CNC Machines Coordinate Tool Movement

A multi-axis CNC machine moves a cutting tool and workpiece through several controlled directions. Three linear axes guide movement along X, Y, and Z. Rotary axes tilt or turn the workpiece. The controller converts programmed coordinates into synchronized servo commands. It also uses inverse kinematics to calculate the correct tool angle. Small timing errors can create visible marks.

Tool center point control keeps the cutter aligned with the programmed path. Look-ahead functions examine upcoming movements before machining begins. This helps the system reduce sudden speed changes and cornering errors. Feedback scales constantly report each axis position. The controller then corrects deviations within milliseconds. That coordination matters when cutting turbine blades, medical components, or deep cavities.

Practical accuracy depends on more than axis count. Thermal growth, fixture movement, tool wear, and vibration can change results. I have seen a clean simulation hide a poor setup. That is worth remembering. A 2024 MarketsandMarkets analysis projects the multi-axis CNC market to grow at about 7.7% annually through 2029. The growth reflects rising demand for fewer setups and tighter process control. However, market forecasts do not guarantee shop-floor performance. Operators still verify tool offsets, collision clearances, and rotary calibration before cutting expensive material. A 2023 report from the U.S. National Institute of Standards and Technology also emphasizes connected measurement and real-time process data for improving manufacturing reliability.

What Is a Multi Axis CNC Machine and How Does It Work? - How Multi-Axis CNC Machines Coordinate Tool Movement

Data Dimension Description How Tool Movement Is Coordinated Typical Production Implication
Basic Definition A multi-axis CNC machine controls several linear and/or rotary axes through computer numerical control. The control system converts programmed coordinates into synchronized axis commands. The cutting tool can approach a workpiece from more than one direction and follow complex toolpaths.
Linear Axes The X, Y, and Z axes provide straight-line movement along three mutually perpendicular directions. Each axis is driven by a servo system, while the CNC control coordinates position, speed, and acceleration. Linear axes establish the tool center point location relative to the workpiece.
Rotary Axes Rotary axes rotate the tool, the workpiece, or both around a defined axis. Rotary position is synchronized with linear movement to maintain the programmed tool orientation and cutting path. Rotary motion can expose multiple faces of a part and support angled or contoured machining.
3-Axis CNC Uses X, Y, and Z linear movement without a continuously controlled rotary axis. The tool position changes in three directions, but the tool orientation normally remains fixed during a cutting operation. Well suited to prismatic parts, pockets, holes, profiles, and many flat or moderately contoured surfaces.
4-Axis CNC Adds one rotary axis to the three primary linear axes. The rotary axis may index the workpiece to a new face or rotate continuously while X, Y, and Z move. Can reduce repositioning for parts with features distributed around a central axis.
5-Axis CNC Combines three linear axes with two rotary axes. The control continuously calculates tool-center-point position and tool-vector orientation as the axes move together. Enables machining of complex surfaces, deep cavities, angled walls, and multiple faces with fewer setups.
Simultaneous vs. Indexed Motion Some machines move multiple axes during cutting, while others position rotary axes between cutting operations. Simultaneous machining coordinates all commanded axes along the active toolpath; indexed machining stops cutting while the orientation changes. Simultaneous motion supports complex 3D surfaces, while indexed motion can simplify programming and inspection.
Tool Center Point Control Tool center point control keeps the programmed cutting point aligned with the intended location on the workpiece. The CNC compensates for rotary-axis movement so the tool tip follows the programmed path when the tool tilts. It helps maintain dimensional accuracy and consistent cutting conditions during multi-axis motion.
Coordinate Transformation The machine must relate the programmed workpiece coordinate system to the moving machine axes. Software applies rotary and linear transformations based on work offsets, tool length, pivot locations, and machine geometry. Accurate machine calibration and correct setup data are essential for reliable results.
CAM Programming Computer-aided manufacturing software generates toolpaths from a digital part model. The CAM system calculates tool positions, feed rates, tilt angles, collision avoidance, and post-processed machine code. More axes can improve access to geometry but generally require more advanced programming and simulation.
Tool Orientation Tool orientation describes the direction in which the cutting tool points relative to the workpiece. Rotary axes continuously or incrementally change the tool angle while linear axes preserve the required contact point. Controlled orientation can improve surface finish, reduce tool interference, and maintain a more favorable cutting angle.
Setup Reduction A multi-axis machine can access several surfaces without manually removing and repositioning the part. The machine changes workpiece orientation or tool direction under programmed control. Fewer setups can reduce alignment errors, handling time, and the need for specialized fixtures.
Collision Management Additional axes create more possible relationships among the tool, holder, machine, fixture, and workpiece. Simulation and machine kinematic models check axis limits, tool-holder clearance, singularities, and potential interference. Verification is especially important before running simultaneous multi-axis programs.
Common Applications Typical applications include impellers, molds, dies, turbine components, medical parts, and complex aerospace structures. The machine coordinates position and orientation to reach surfaces that are difficult to access with fixed-axis cutting. The main value is improved access, fewer setups, and the ability to produce intricate geometries.
Key Limitations Multi-axis systems are generally more complex to purchase, program, operate, calibrate, and maintain than simpler machines. Errors in kinematic data, post-processing, rotary-axis positioning, or tool measurement can affect the final part. The productivity benefit should be evaluated against programming time, operator training, tooling, and inspection requirements.

Common Multi-Axis Configurations and Their Differences

A multi-axis CNC machine moves a cutting tool and workpiece along several coordinated directions. Linear axes control left-right, forward-back, and vertical movement. Rotary axes tilt or rotate the part. The controller combines these movements through programmed coordinates. This allows one setup to reach complex surfaces, holes, and angled edges.

Common configurations differ in flexibility and control difficulty. A three-axis machine cuts from fixed tool directions and suits flat or moderately shaped parts. A three-plus-one machine adds a rotary positioning axis, but usually stops rotation during cutting. A four-axis machine can rotate the workpiece while cutting, making it useful for shafts, housings, and repeated side features. A five-axis machine adds another rotary movement. It can keep the tool normal to curved surfaces and reduce multiple setups. However, programming becomes harder, and collision checking matters more. More axes are not automatically better. That assumption deserves review.

Tips: Match the configuration to the part, not the sales description. Check the machine’s real travel, rotary limits, and spindle access. Use simulation before cutting metal. Small angular errors can leave visible marks on a curved surface. A stable setup still matters. Even advanced equipment cannot correct weak fixturing or unclear tolerances.

Typical Applications, Benefits, and Operating Challenges

A multi-axis CNC machine moves a cutting tool along several coordinated directions. Some systems add rotary motion through tilting heads or rotary tables. This allows one setup to reach angled faces, deep pockets, and curved surfaces. In aerospace, medical, mold, and energy work, that access can reduce handling. A part may leave the machine nearly complete. That matters.

Typical applications include impellers, turbine components, orthopedic parts, complex molds, and prototype housings. Multi-axis cutting improves positional consistency because fewer setups mean fewer alignment errors. It can also shorten cycle time and reduce fixture costs. Better tool orientation often improves surface finish and tool life. The payoff is real. However, savings depend on programming quality, tooling, and machine condition.

Operating challenges begin before the spindle starts. Engineers must check collision risks, tool reach, workholding, post-processor accuracy, and material behavior. A small fixture mistake can damage an expensive workpiece. Programs also demand simulation and careful verification on the shop floor. Five-axis motion may look elegant, but it is not automatically faster. Poor toolpaths can create hesitation marks, heat, or wasted motion. Operators need training in coordinate systems and rotary-axis limits. Even experienced teams can miss a hidden singularity. That deserves another check.

What Is a Multi-Axis CNC Machine and How Does It Work?

Multi-axis CNC machines coordinate linear and rotary motion to machine multiple surfaces in a single setup. The chart shows common axis configurations and the number of linear and rotary axes they typically provide.

Key point: A standard 3-axis machine moves along X, Y, and Z. A 4-axis machine adds one rotary axis, while a 5-axis machine typically adds two rotary axes, enabling access to complex surfaces and reducing repositioning. More axes can improve flexibility and reduce setups, but they also increase programming, calibration, collision-control, and operator-training requirements.

Certified Quality System

© North Easton Machine Company, Inc. All rights reserved. • Site: Blog
NORTH EASTON MACHINE • 218 Elm Street • North Easton, MA 02356 • 508-238-6219