How to Choose the Best Filament for 3D Printing
Choosing a 3D printing Filament is not just a matter of picking a color. The material affects strength, flexibility, surface finish, print temperature, and how reliably a part performs. A spool that feeds smoothly through a printer may still produce a brittle bracket or a warped, lifting corner. Small details matter.
The Wohlers Report 2024 estimated that the global additive manufacturing industry generated $20.035 billion in revenue in 2023. That figure includes more than filament alone, but it shows how quickly professional and desktop 3D printing are expanding. As more materials enter the market, choosing by price or popularity alone becomes less dependable. Dr. Joshua Pearce, a researcher in open-source 3D printing, has emphasized the practical value of accessible, locally produced manufacturing. In that spirit, material choice should start with the part’s real job—not the label on the spool.
Think about the conditions your print will face. Will it sit in a hot car, flex repeatedly, or hold a screw under load? PLA is often easy to print and gives crisp details, while PETG can offer more toughness and heat resistance. Nylon may suit demanding parts, but moisture can complicate printing. Trade-offs are unavoidable. Even a well-matched Filament can disappoint if it is damp, poorly stored, or printed with unsuitable settings. The right choice is usually a balance, not a perfect answer. Consider the printer, the use case, and your tolerance for failed prints before committing to a material.
Define the Purpose and Performance Needs of the Printed Part
A filament choice starts with the part’s job, not its color. Will it hold a load, flex repeatedly, touch warm surfaces, or simply sit on a shelf? A decorative model may need clean detail and a smooth finish. A working bracket needs strength, dimensional accuracy, and resistance to its real surroundings. Looks are not enough.
Write down the expected force, temperature, moisture exposure, and fit before comparing materials. PLA can suit many indoor prototypes and display pieces, while PETG often handles impact and damp conditions better. Nylon may work for wear or repeated flexing, but moisture control and print setup matter. No material is universally best. A part inside a hot vehicle, for example, may soften if its heat resistance is too low.
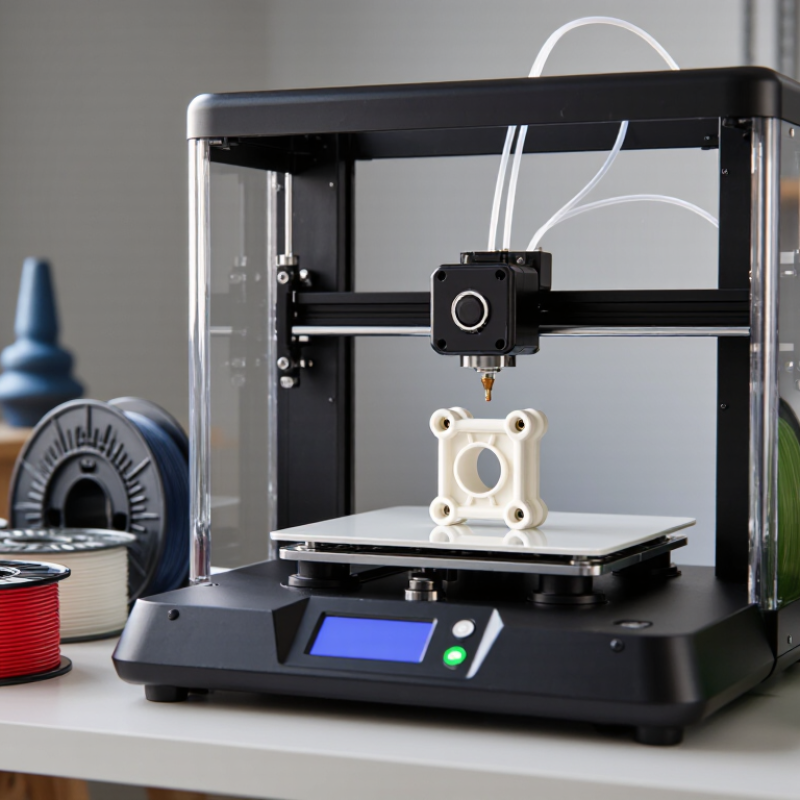
I have seen sturdy-looking prints crack at thin screw holes, where stress concentrates. That surprised me. Check wall thickness, layer direction, and how the part will be fastened; these details can matter as much as the filament. If the load is uncertain, print a small test piece and try it under realistic conditions. Keep a margin. Record what failed, too, because a quick test cannot predict every use.
How to Choose the Best Filament for 3D Printing - Define the Purpose and Performance Needs of the Printed Part
| Filament | Best Suited For | Typical Printed Tensile Strength | Heat and Environmental Performance | Key Trade-Offs |
| PLA | Decorative models, prototypes, fixtures, and parts used indoors under light loads. | Approximately 45–60 MPa | Low heat resistance; parts can soften in hot environments or a sun-heated vehicle. | Easy to print and generally dimensionally stable, but comparatively brittle and unsuitable for sustained heat or heavy-duty use. |
| PETG | Functional household parts, covers, brackets, and components that need more impact resistance than PLA. | Approximately 40–55 MPa | Moderate heat resistance and good resistance to moisture; useful for many indoor and sheltered outdoor applications. | Tough and less brittle than PLA, but can string during printing and may flex more under load. |
| ABS | Durable housings, enclosures, and parts that may experience impact or moderate heat. | Approximately 30–45 MPa | Better heat resistance than PLA or PETG; not inherently resistant to prolonged UV exposure. | Can warp or shrink while printing and may require an enclosure and good ventilation. |
| ASA | Outdoor brackets, covers, fixtures, and other parts exposed to sunlight and changing weather. | Approximately 35–50 MPa | Good UV and weather resistance, with heat performance broadly comparable to ABS. | Offers outdoor durability, but can warp during printing and benefits from an enclosed, ventilated setup. |
| TPU | Flexible grips, bumpers, seals, protective cases, and parts that need to bend or absorb impact. | Approximately 20–50 MPa, depending strongly on hardness and formulation | Flexible across a wide range of uses; heat and chemical resistance vary by formulation. | Highly elastic and abrasion-resistant, but prints slowly and can be difficult to feed through some printers. |
| Nylon (PA) | Wear-resistant functional parts such as gears, hinges, bushings, and clips. | Approximately 45–85 MPa, depending on type and print direction | Good abrasion resistance and toughness; absorbs moisture, which can affect dimensions and print quality. | Strong and durable, but requires careful moisture control and can warp during printing. |
| Polycarbonate (PC) | Strong functional components that need high impact strength and better heat resistance. | Approximately 55–75 MPa | High heat resistance among common desktop-printing materials; performance depends on the specific formulation. | Can be demanding to print, often needing a high-temperature setup, an enclosure, and dry filament. |
Note: Strength figures are approximate ranges for printed parts, not guaranteed material specifications. Results vary with filament formulation, printer settings, part geometry, and layer orientation. Choose based on the part’s actual load, temperature, moisture, UV exposure, and flexibility requirements.
Compare Filament Types by Strength, Flexibility, and Heat Resistance
Choosing filament means balancing strength, flexibility, and heat resistance rather than chasing one “best” material. PLA is stiff and easy to print, making it suitable for brackets or display parts that stay cool. It can crack under sharp impact and soften in a hot car. PETG bends a little more and often handles knocks better, though thin features may still flex too much. Test a small part.
For warmer environments, ABS and ASA generally tolerate more heat than PLA, but they can warp during printing. A stable enclosure and good ventilation help manage the process. Nylon can make tough, wear-resistant parts, yet it absorbs moisture from the air; damp filament may print with a rough, bubbly surface. Dry storage matters. TPU is the flexible choice for grips, feet, or protective covers. Its softness is useful, but it is not a substitute for a rigid load-bearing part.
Compare samples under realistic conditions. Print the same small hook in two materials, then check how it bends and whether it returns to shape. For heat, test a spare piece near the part’s expected operating temperature, not over an open flame. I would not trust a single quick test for a safety-critical component. Even familiar filaments can behave differently with wall thickness, print direction, and moisture. Choosing is a little messier than a spec sheet suggests.
How to Choose the Best Filament for 3D Printing
Compare typical strength, flexibility, and heat resistance. Start with the properties your part needs most.
The chart shows approximate tensile-strength ranges for FDM-printed parts as representative values. Actual results vary with print orientation, settings, filament formulation, and test method.
| Filament | Typical flexibility | Typical heat resistance | Good fit for |
| PLA | Low; brittle compared with other options | Low; heat deflection often around 50–60°C | Rigid prototypes and indoor parts |
| PETG | Moderate; tougher and less brittle than PLA | Moderate; often around 65–80°C | General-purpose parts needing toughness |
| ABS | Moderate; can flex before breaking | Higher; often around 85–105°C | Functional parts exposed to warmth |
| Nylon (PA) | Moderate to high; grade-dependent | Moderate to high; grade-dependent | Wear-resistant parts and durable fixtures |
| TPU | Very high; elastomeric | Usually low to moderate; grade-dependent | Flexible grips, bumpers, and seals |
| Polycarbonate (PC) | Moderate; tough, grade-dependent | High; many grades soften above 110°C | Strong parts needing higher heat tolerance |
Heat figures are approximate and depend on the specific grade and test method. Check the filament’s technical data sheet when a part has strict strength or temperature requirements.
Check Printer Compatibility and Required Printing Conditions
Before choosing a filament, check what your printer can safely handle. The hotend must reach the material’s recommended nozzle temperature, and the build plate must support its bed temperature. A printer limited to lower temperatures may struggle with some engineering plastics. Check the manufacturer’s specifications, not just the temperature shown on the screen.
The extruder matters too. Flexible filament can bend or buckle in a long, unsupported feed path, while abrasive blends may wear a standard nozzle faster. Check the filament diameter your printer accepts; a mismatch can cause uneven feeding. Small details count.
Think about the printing environment. Some materials benefit from an enclosure to reduce drafts and temperature changes. Others need a dry storage box because moisture can cause popping sounds, rough surfaces, or weak layers. Ventilation is worth considering, especially when a material’s safety guidance recommends it. Read the spool label and its technical data sheet.
It is easy to focus on strength and overlook printer limits. I would check compatibility before buying, then test with a small, simple print. Even good specifications cannot predict every machine’s quirks. A first print may still need adjustment.
Balance Material Cost, Ease of Use, and Surface Finish
How to Choose the Best Filament for 3D Printing
Balance Material Cost, Ease of Use, and Surface Finish
Filament choice is a three-way trade-off: spool price, printing effort, and the look of the finished part. Grand View Research estimated the global 3D-printing plastics market at USD 1.7 billion in 2023, reflecting growing use across applications. But a cheaper spool is not automatically the cheaper print. A few failed jobs can erase the saving. That matters.
PLA is often an approachable starting point: it prints at relatively low temperatures and can leave crisp details on a small desk model. PETG can suit parts needing more toughness, though stringing may require slower settings and extra cleanup. For a smooth surface, test a short sample before committing to a large object. Layer height, cooling, and nozzle condition can change the result as much as the material. I still overestimate how much a premium finish will hide rough settings. It won’t.
Wohlers Report 2024 put global additive-manufacturing revenue at about USD 20.0 billion in 2023, up 11.1% from 2022. That broad growth makes practical material selection more relevant, not less. Compare cost per usable part, not just cost per kilogram; include drying, failed prints, and finishing time. A matte surface may disguise fine layer lines, while glossy filament can make them more visible. Not always. Keep notes on temperature, speed, and finish for each spool, then compare the same small test shape.
Test a Suitable Filament and Refine the Printing Settings
Before committing to a full print, test the filament on a small, repeatable part. A simple cube with a bridge and a few overhangs reveals several common problems. Start within the temperature range suggested for the material, then print samples at small temperature intervals. Change only one setting at a time. This makes cause and effect easier to judge. Keep notes.
Look closely at the results, not just the surface. Fine hairs between posts may indicate excess heat or moisture; weak layers can suggest a temperature that is too low. Warped corners often point to poor bed adhesion, drafts, or insufficient bed heat. Dry the filament when its material guidance recommends it, and store it sealed between tests. Then adjust speed, cooling, or bed temperature in modest steps. A setting that works on a tiny sample may fail on a tall part, so test a representative shape before relying on it. I have found that a neat first layer can still hide brittle walls. Be willing to revisit the settings.
 Find Your Solutions ▶